Перейти к содержанию
Coenzyme Q10 is essential for cellular energy and high-demand supplements. However, sourcing pure, stable CoQ10 amidst global supply chain risks can be challenging. This guide explains why fermentation-grade CoQ10 is critical, how to protect ingredient stability, and ways to use water-soluble CWD technology for superior formulations.
Understanding Fermentation-Grade CoQ10 vs. Synthetic Alternatives
Sourcing high-quality CoQ10 powder begins with understanding its production method. The preferred industry standard is biological yeast or bacterial fermentation. This natural process yields the all-trans isomer of Coenzyme Q10, a molecular structure identical to the CoQ10 produced naturally inside the human body.
In contrast, synthetic production relies on chemical synthesis, which often creates unwanted cis-isomer impurities. The human body does not efficiently recognize or utilize these cis-isomers, making synthetic alternatives less effective for nutritional supplementation. Furthermore, residual solvents from chemical synthesis can introduce safety concerns. Fermentation-derived extraction avoids these risks entirely.
Purity Advantages for Demanding Applications
Fermentation-derived CoQ10 consistently achieves the exceptional purity levels required for demanding pharmaceutical formulas and functional food applications. SOHO Honry Chemical utilizes advanced testing equipment to verify this purity. Our R&D team ensures ingredients meet strict Eurofin and SGS standards, guaranteeing a safe, reliable active ingredient.
| Особенность | Fermentation-Grade CoQ10 | Synthetic CoQ10 |
|---|---|---|
| Production Method | Biological yeast or bacterial fermentation | Chemical synthesis |
| Молекулярная структура | All-trans isomer | Mix of trans and cis-isomers |
| Biological Compatibility | High (matches human biology) | Lower (body rejects cis-isomers) |
| Impurity Profile | Minimal to none | Potential residual solvents |
Aligning with Clean-Label Market Trends
Modern consumers expect transparent, clean-label ingredients. Fermentation naturally aligns with these trends, providing a natural sourcing origin that synthetic alternatives cannot match. Biological fermentation easily meets stringent natural and NON-GMO formulation requirements.
Our production facilities hold comprehensive certifications to support these demands, including HALAL, KOSHER, NON-GMO, and ALLERGEN FREE. Using certified fermentation-grade ingredients helps brands build consumer trust while maintaining strict regulatory compliance.
Key Stability Factors for CoQ10 Powder in Manufacturing
Coenzyme Q10 is highly sensitive to its environment. During manufacturing, light, heat, and oxygen pose severe threats to its stability. Exposure to UV light triggers rapid photo-degradation, oxygen contact leads to unwanted oxidation, and high heat quickly breaks down the molecular structure. These factors can compromise the ingredient before it reaches the final product.
Managing Supply Chain and Storage Risks
Global supply chain risks make temperature control a top priority. Moving ingredients across borders exposes them to extreme climate shifts. Fluctuating temperatures during transit and warehousing accelerate active ingredient degradation, significantly shortening shelf life. Maintaining strict climate-controlled logistics is essential for preserving chemical potency.
Proper handling protocols are just as critical as storage conditions. Manufacturers should conduct regular physical inventory valuation and rotate stock to ensure older batches are processed before degradation occurs. Strict handling guidelines prevent unnecessary exposure when opening bulk containers. SOHO Honry Chemical supports these efforts with rigorous quality control inside our GMP and ISO-certified facilities.
Practical Steps for Ingredient Protection
Manufacturers must implement strong defenses to protect this sensitive compound during formulation. Standard protection strategies include:
- Microencapsulation: Используя water soluble CoQ10 (CWD) technology wraps the active molecule in a protective matrix. This shields it from direct oxygen and light.
- Opaque Packaging: Storing raw materials in dark, airtight containers prevents UV and oxygen damage.
- Climate Control: Processing areas should always maintain strict temperature and humidity parameters.
Exploring Water Soluble CoQ10 and CWD Technology
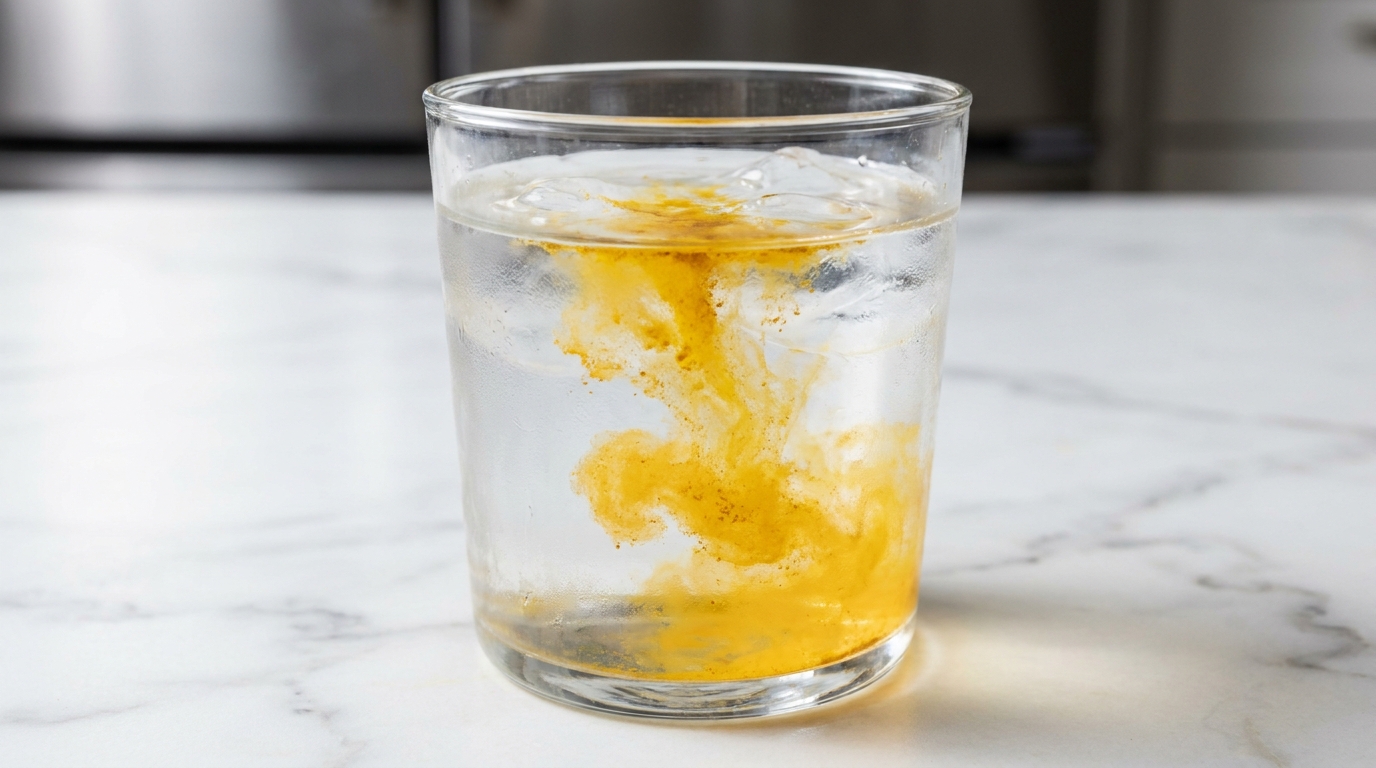
Standard CoQ10 is naturally lipophilic, meaning it dissolves in fat rather than water. This characteristic presents a significant hurdle for manufacturers, as it limits direct absorption in the human digestive tract and prevents the raw ingredient from mixing easily into water-based formulas. Traditional softgels often rely on carrier oils to address this issue, but this restricts product variety.
Water-soluble formulations offer a highly bioavailable alternative. By modifying how the compound interacts with liquids, manufacturers can overcome traditional absorption barriers. This expanded versatility allows formulators to create diverse product formats that meet modern consumer preferences.
The Mechanics of CWD Processing
Cold Water Dispersible (CWD) technology is the primary driver behind this innovation. CWD processing transforms standard CoQ10 into a fine, highly stable powder that disperses rapidly and evenly in ambient or cold water.
Crucially, the dispersion process does not require high temperatures. Avoiding heat protects the sensitive active ingredient from thermal degradation. The resulting microencapsulated structure also helps shield the CoQ10 from oxygen and light exposure during manufacturing.
Modern Applications for CWD Formulations
CWD technology opens new doors for consumer-friendly nutritional products. Formulators can seamlessly integrate water-soluble CoQ10 into several high-demand categories:
- Functional Beverages: CWD powder mixes cleanly into ready-to-drink formulas. It prevents gritty textures and unsightly oily separation.
- Liquid Supplements: Enhanced solubility ensures consistent active ingredient distribution. This provides a smooth, uniform texture in concentrated drops and syrups.
- Gummy Candies: Water-soluble ingredients blend evenly into pectin or gelatin bases. SOHO Honry Chemical actively supports leading companies in developing stable gummy candy and beverage formulations.
| Formulation Feature | Standard CoQ10 Powder | CWD Water-Soluble CoQ10 |
|---|---|---|
| Solubility Profile | Fat-soluble (lipophilic) | Water-dispersible (hydrophilic behavior) |
| Ideal Product Formats | Softgels, oil suspensions, standard tablets | Beverages, liquid drops, gummies, effervescents |
| Bioavailability | Requires dietary fats for optimal absorption | Enhanced for direct absorption |
| Processing Requirements | May require gentle warming to blend with oils | Mixes readily in cold or ambient water |
Essential Quality Standards and Certifications in CoQ10 Sourcing
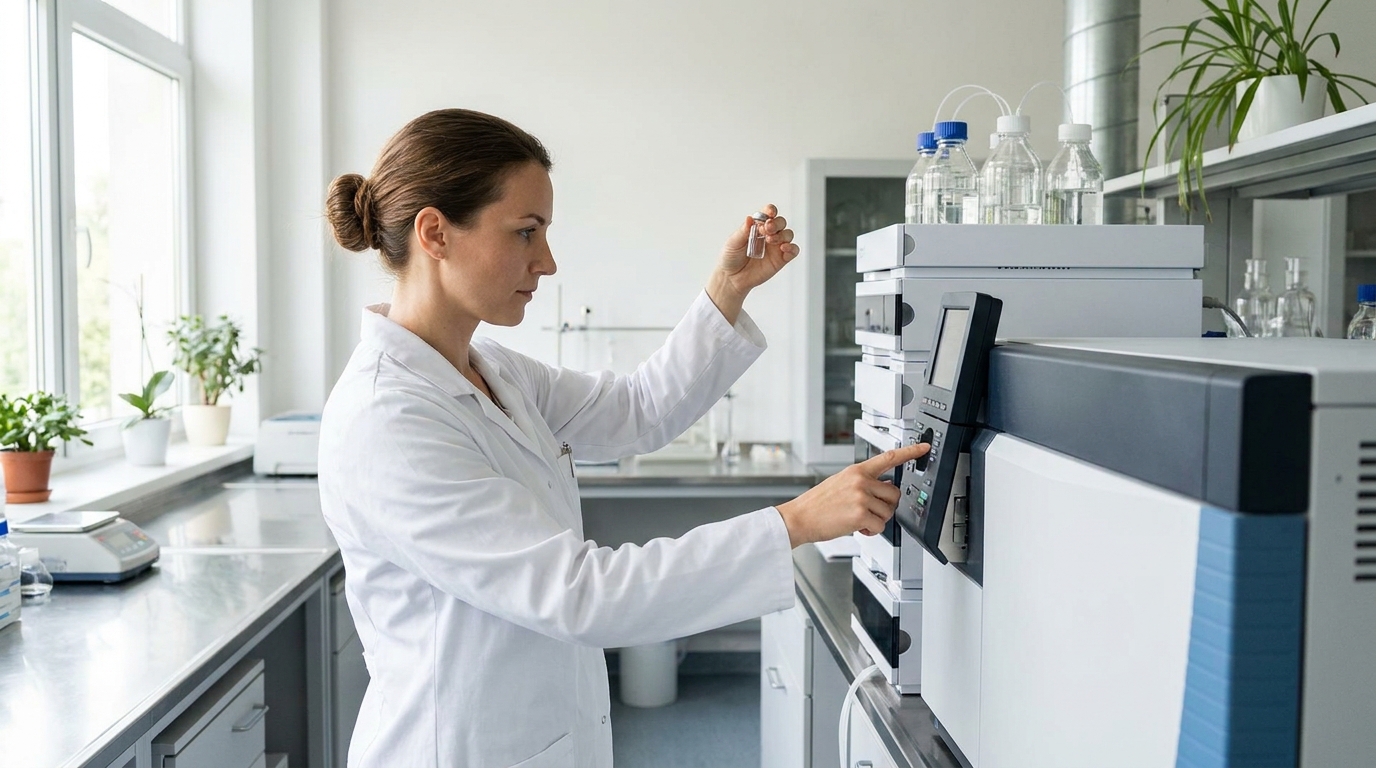
Sourcing high-quality CoQ10 requires strict adherence to global manufacturing standards. Facility certifications prove a supplier’s commitment to safety and operational excellence. Buyers should partner with facilities that hold comprehensive credentials to ensure the manufacturing environment meets rigorous hygiene and process control benchmarks.
Critical facility certifications to require include:
- FSSC and BRC: Demonstrate advanced food safety and supply chain management systems.
- ISO: Ensures consistent quality management across all operational levels.
- GMP: Guarantees products are consistently produced and controlled according to strict quality standards.
SOHO Honry Chemical operates under these exact standards. Our certified facilities maintain strict environmental controls to protect sensitive ingredients from degradation risks.
Product-Level Credentials for Global Markets
Beyond facility operations, the ingredient itself must meet diverse consumer demands. Formulators need raw materials that comply with specific dietary and ethical requirements. Securing product-level certifications is crucial for global market access. Essential credentials include HALAL, KOSHER, NON-GMO, and ALLERGEN FREE statuses. These labels allow brands to confidently formulate supplements for broader demographics without facing regulatory hurdles.
Third-Party Auditing and Batch Testing
Internal quality checks are necessary, but independent verification provides ultimate supply chain transparency. Reliable suppliers submit to annual third-party audits to maintain their facility credentials. They also test ingredient batches against internationally recognized benchmarks, such as Eurofin and SGS standards. This rigorous testing verifies the purity and potency of the active compound before it leaves the warehouse.
At SOHO Honry Chemical, our R&D team includes over 25 technicians led by two PhDs. In collaboration with top institutions like China Pharmaceutical University, we utilize advanced testing equipment to provide comprehensive analytical reports. To learn more about our commitment to scientific health and innovation, you can read about us and our robust quality control systems.
Strict Quality Control Protocols
Consistent active ingredient concentration is vital for product efficacy. Strict quality control protocols prevent cross-contamination during manufacturing, handling, and packaging. Thorough equipment sanitation and controlled handling procedures eliminate the risk of unwanted residues. By enforcing these protocols, manufacturers can guarantee that every batch delivers the exact CoQ10 dosage required for the final formulation.
Mitigating Supply Chain Risks in the Nutraceutical Market
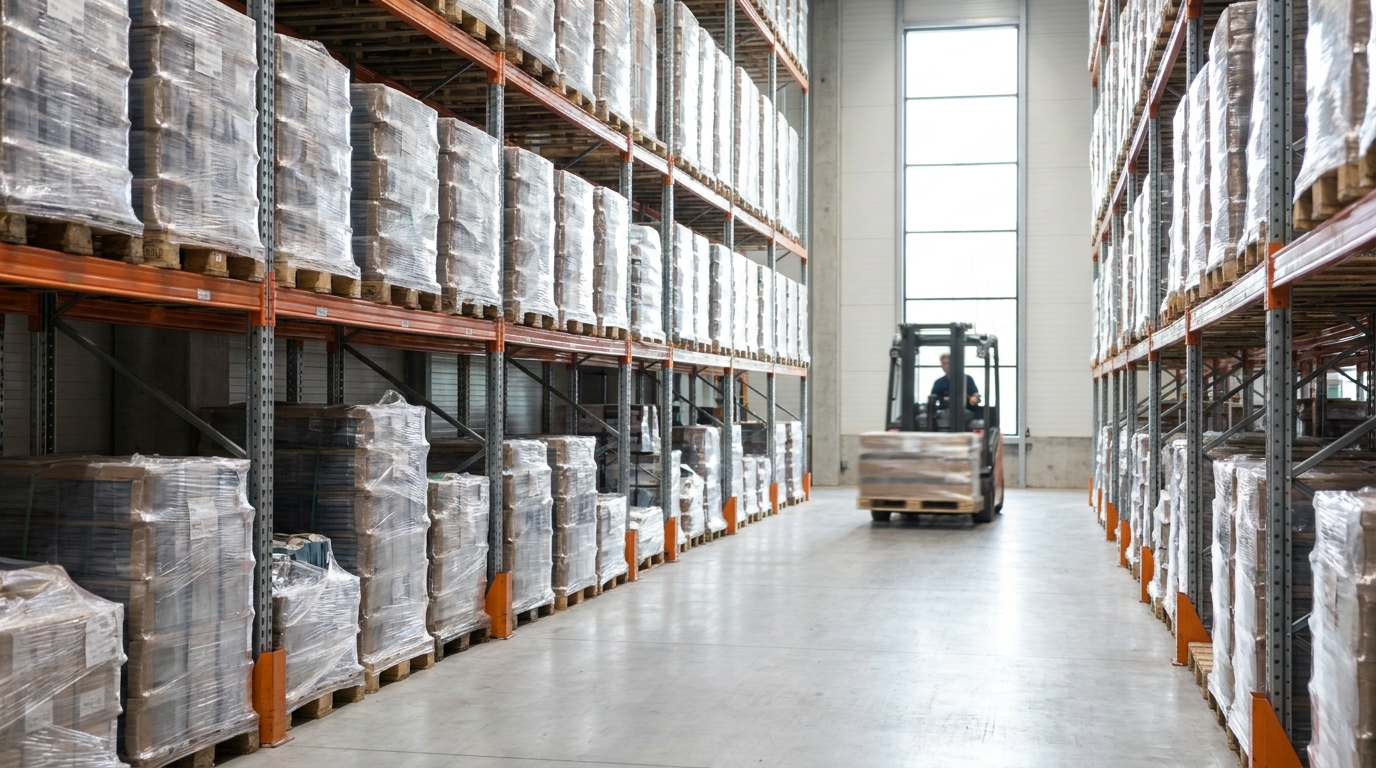
Sourcing nutritional ingredients like CoQ10 powder involves navigating a complex global market. Buyers face frequent demand-supply gaps and raw material volatility. Geopolitical events and economic shifts often disrupt specialty chemical and pharmaceutical API sectors, directly impacting the availability and pricing of essential nutraceuticals.
Navigating this opacity requires accurate data. Relying on outdated market research reports is a critical mistake, as global chemical markets are highly dynamic and unpredictable. Procurement teams must continuously track supply chain shifts and production levels. Near-real-time updates on API prices help manufacturers optimize procurement costs and avoid sudden ingredient shortages.
Strategies for Consistent Ingredient Sourcing
To maintain supply chain stability, manufacturers must adopt proactive procurement strategies. Relying on a single source creates significant operational vulnerabilities. Implementing diverse purchasing tactics helps mitigate these risks.
- Diversify Sourcing Regions: Expand procurement networks across multiple geographic regions. This buffers against localized trade disruptions and regional material shortages.
- Secure Term Contracts: Spot market purchases expose buyers to sudden price spikes. Establishing term contracts with reliable manufacturers locks in pricing and guarantees volume.
- Continuous Price Tracking: Monitor agricultural feedstock and specialty chemical markets daily. Recognizing early trend shifts allows buyers to adjust purchasing volumes before prices peak.
| Procurement Strategy | Primary Advantages | Supply Chain Impact |
|---|---|---|
| Spot Market Purchasing | Flexibility to capitalize on sudden price drops. | High exposure to market volatility and potential stockouts. |
| Long-Term Contracts | Predictable pricing and guaranteed supply volumes. | Stabilizes production schedules and protects profit margins. |
| Supplier Diversification | Reduces dependence on single manufacturing regions. | Prevents complete operational halts during geopolitical events. |
Protecting Margins Through Operational Efficiency
Effective inventory management is another crucial defense mechanism. Proactive physical inventory valuation helps protect profit margins during periods of economic uncertainty. By understanding exact stock levels, manufacturers can avoid over-purchasing during price surges.
Furthermore, buyers must evaluate a supplier’s operating efficiency before committing to contracts. Partnering with highly efficient suppliers minimizes unexpected delays. SOHO Honry Chemical leverages a robust global supply chain to ensure consistent ingredient delivery. Our advanced equipment and dedicated technical team help keep client production lines moving seamlessly, even during turbulent market conditions.
Partnering with a Reliable Global Ingredients Solution Supplier
Securing a stable supply of CoQ10 powder requires more than just placing orders. Brands need partners who integrate advanced research and development with large-scale manufacturing. This integration ensures that theoretical formulations successfully transition into commercial production. Suppliers operating GMP-certified facilities can scale up production while maintaining strict quality standards.
The Value of Academic Collaboration
Ingredient innovation thrives through dedicated academic collaboration. Leading suppliers often partner with top research institutions to refine their manufacturing techniques. SOHO Honry Chemical maintains deep cooperation with universities such as Nanjing Agricultural University and China Pharmaceutical University. These partnerships allow us to leverage cutting-edge scientific health research, translating into more stable, highly bioavailable ingredients for our clients.
Expert Technical Support for Custom Formulations
Developing specialized products often requires custom formulation support. Overcoming solubility challenges with water-soluble CoQ10 or applying CWD technology demands expert guidance. Our R&D team, which includes over 25 technicians led by two PhDs, provides hands-on support for diverse production applications. We actively assist clients across the human nutrition, food and beverage, and personal care sectors.
Ensuring Safe and Competitive Solutions
Ultimately, a supplier’s value lies in the safety and competitiveness of the final product. Comprehensive testing capabilities verify that ingredients consistently meet exact physical specifications. By combining strict facility credentials with advanced analytical testing, manufacturers effectively mitigate ongoing procurement risks. This comprehensive approach empowers global brands to confidently deliver safe, competitive, and healthy product solutions to consumers.
Frequently Asked Questions About Coenzyme Q10 Sourcing
What is the difference between fermentation-grade and synthetic CoQ10?
Fermentation-grade CoQ10 is produced using biological yeast or bacteria, creating an all-trans isomer that perfectly matches the CoQ10 found naturally in the human body. This makes it highly effective and easily absorbed. In contrast, synthetic CoQ10 is made through chemical synthesis. This process often leaves behind unwanted cis-isomers that the body struggles to use, and it carries the risk of containing residual chemical solvents.
Why should I choose water-soluble CoQ10 for my formulations?
Standard CoQ10 is naturally fat-soluble, meaning it does not mix well with water and has lower direct absorption in the digestive tract. Water-soluble CoQ10 uses Cold Water Dispersible (CWD) technology to microencapsulate the active molecule. This allows the powder to dissolve quickly and evenly in cold or room-temperature liquids. It is the ideal choice for creating functional beverages, liquid drops, gummy candies, and effervescent tablets without oily separation.
How should CoQ10 powder be stored to prevent degradation?
CoQ10 is highly sensitive to light, heat, and oxygen. To protect the active ingredient, it must be stored in dark, airtight, and opaque packaging to block UV light and oxygen exposure. Facilities should also maintain strict temperature and humidity controls. During manufacturing and transit, maintaining a climate-controlled environment is critical to prevent the compound from breaking down and losing its potency before it reaches the final product.
What quality certifications are essential when sourcing CoQ10?
A reliable CoQ10 supplier should hold major facility certifications like GMP, ISO, FSSC, and BRC to guarantee strict manufacturing and hygiene standards. Additionally, you should look for product-level credentials such as HALAL, KOSHER, NON-GMO, and ALLERGEN FREE. SOHO Honry Chemical meets all these standards and relies on third-party testing against Eurofin and SGS benchmarks to guarantee the highest purity and safety for global markets.
How can buyers protect against CoQ10 supply chain shortages?
Global chemical and ingredient markets can be highly unpredictable due to geopolitical events and shifting demands. To prevent shortages, buyers should avoid relying on a single supplier and instead diversify their sourcing regions. Securing long-term contracts rather than relying on spot market purchases helps lock in pricing and guarantees supply volumes. Finally, continuously tracking market trends and API prices allows procurement teams to adjust their purchasing strategies before price spikes occur.
Заключение
Sourcing fermentation-grade CoQ10 ensures high purity and stability for your formulations. Utilizing advanced formats like water-soluble and CWD technology allows for versatile product development. To protect your supply chain, partner with a transparent, certified supplier backed by robust R&D.
- Verify supplier facility certifications like GMP, FSSC, and BRC.
- Request third-party testing reports matching Eurofin or SGS standards.
- Ask about custom water-soluble CoQ10 solutions for your product.